Case study · Manufacturing
PE firm's manufacturing holding cuts $6M a year and creates $36M in value
A private equity firm's manufacturing holding, built by acquisition, ran on disparate systems that hid its true capacity. USC found the hidden capacity, guided a plant consolidation and installed a closed-loop management operating system.
Results
$6M
in annualized cost savings
$36M
in value created
22%
reduction in scrap
Savings are annualized; value created is approximate.
The situation
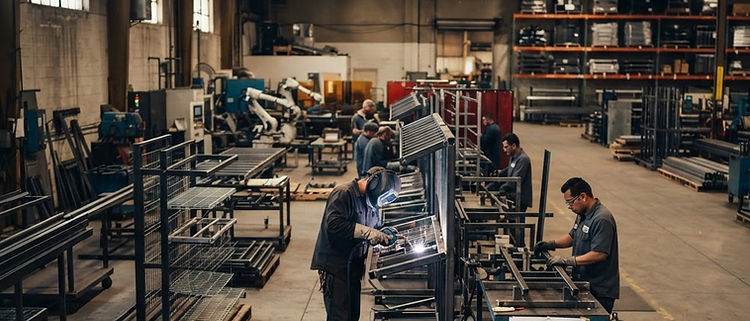
The holding made metal display racks for big-box retailers and ran warehousing and distribution. Assembled through acquisitions, it ran on several disparate systems, leaving its true production capacity unclear. The firm wanted asset utilization, throughput, setup time and scrap improved quickly.
What the assessment found
- Hidden capacity across the network, masked by disparate systems
How the work was done
Footprint: consolidate plants
Built the financial analysis and critical path for which plants to consolidate and in what order, with loading profiles, safety stock and order-transfer plans.
Execution: track every action
Ran more than 200 action items by functional area through biweekly owner reviews and weekly steering team reviews.
Operations: close the loop
Installed a management operating system giving visibility, traceability and accountability for every customer order.
16%
increase in productivity
“What we initially thought couldn't be done USCCG accomplished and, in the process, created substantial additional value across the combined enterprise.”
Lasting impact
The holding moved from five locations to four without disrupting service to its major customers, improving EBITDA. Annual cost fell $6 million and the investment gained about $36 million in value.
Related case studies
Manufacturing
Control systems maker adds $1.5M annual revenue, cuts labor cost per job 51%
$1.5Mincrease in annual revenue
Read the case study →Manufacturing
Pulp and paper maker cuts bleach chemical costs $2M a year at one mill
$2Min annual bleach chemical savings at one mill
Read the case study →Manufacturing
Controls manufacturer saves $500K a year by streamlining order-to-cash
$500K+in annual back-office savings
Read the case study →